PCBs The Prehistoric Way

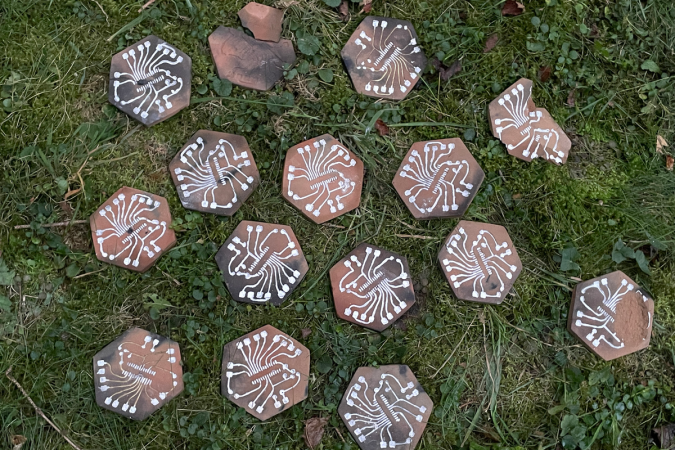
When we see an extremely DIY project, you always get someone who jokes “well, you didn’t collect sand and grow your own silicon”. [Patrícia J. Reis] and [Stefanie Wuschitz] did the next best thing: they collected local soil, sieved it down, and fired their own clay PCB substrates over a campfire. They even built up a portable lab-in-a-backpack so they could go from dirt to blinky in the woods with just what they carried on their back.

This project is half art, half extreme DIY practice, and half environmental consciousness.  (There’s overlap.)  And the clay PCB is just part of the equation. In an effort to approach zero-impact electronics, they pulled ATmega328s out of broken Arduino boards, and otherwise “urban mined” everything else they could: desoldering components from the junk bin along the way.

The traces themselves turned out to be the tricky bit. They are embossed with a 3D print into the clay and then filled with silver before firing. The pair experimented with a variety of the obvious metals, and silver was the only candidate that was both conductive and could be soldered to after firing. Where did they get the silver dust? They bought silver paint from a local supplier who makes it out of waste dust from a jewelry factory. We suppose they could have sat around the campfire with some old silver spoons and a file, but you have to draw the line somewhere. These are clay PCBs, people!

Is this practical? Nope! It’s an experiment to see how far they can take the idea of the pre-industrial, or maybe post-apocalyptic, Arduino. [Patrícia] mentions that the firing is particularly unreliable, and variations in thickness and firing temperature lead to many cracks. It’s an art that takes experience to master.

We actually got to see the working demos in the flesh, and can confirm that they did indeed blink! Plus, they look super cool. The video from their talk is heavy on theory, but we love the practice.

DIY clay PCBs make our own toner transfer techniques look like something out of the Jetsons.
Continue reading “PCBs The Prehistoric Way” →

Camera And ChArUco Keep The Skew Out Of Your 3D Prints

Do you or a loved one suffer from distorted 3D prints? Does your laser cutter produce parallelograms instead of rectangles? If so, you might be suffering from CNC skew miscalibration, and you could be entitled to significant compensation for your pain and suffering. Or, in the reality-based world, you could simply fix the problem yourself with this machine-vision skew correction system and get back to work.

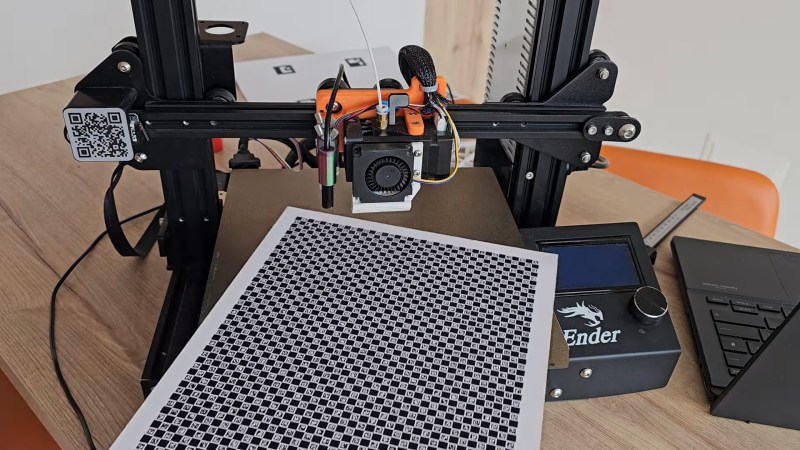
If you want to put [Marius Wachtler]’s solution to work for you, it’s probably best to review his earlier work on pressure-advance correction. The tool-mounted endoscopic camera he used in that project is key to this one, but rather than monitoring a test print for optimum pressure settings, he’s using it to detect minor differences in the X-Y feed rates, which can turn what’s supposed to be a 90-degree angle into something else.

The key to detecting these problems is the so-called ChArUco board, which is a hybrid of a standard chess board pattern with ArUco markers added to the white squares. ArUco markers are a little like 2D barcodes in that they encode an identifier in an array of black and white pixels. [Marius] provides a PDF of a ChArUco that can be printed and pasted to a board, along with a skew correction program that analyzes the ChArUco pattern and produces Klipper commands to adjust for any skew detected in the X-Y plane. The video below goes over the basics.

For as clever and useful as ChArUco patterns seem to be, we’re surprised we haven’t seen them used for more than this CNC toolpath visualization project (although we do see the occasional appearance of ArUco). We wonder what other applications there might be for these boards. OpenCV supports it, so let us know what you come up with.

Continue reading “Camera And ChArUco Keep The Skew Out Of Your 3D Prints” →

No Need For Inserts If You’re Prepared To Use Self-Tappers

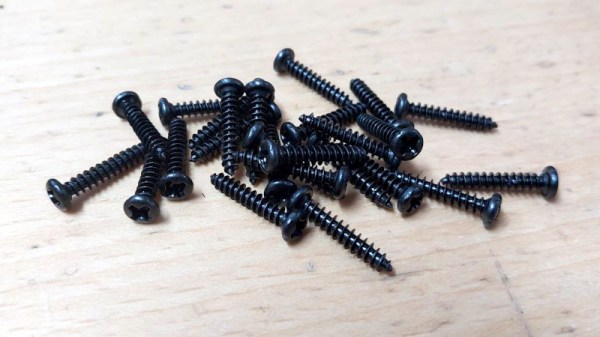
As the art of 3D printing has refined itself over the years, a few accessories have emerged to take prints to the next level. One of them is the threaded insert, a a piece of machined brass designed to be heat-set into a printed hole in the part. They can be placed by hand with a soldering iron, or for the really cool kids, with a purpose-built press. They look great and they can certainly make assembly of a 3D printed structure very easy, but I’m here to tell you they are not as necessary as they might seem. There’s an alternative I have been using for years which does essentially the same job without the drama. Continue reading “No Need For Inserts If You’re Prepared To Use Self-Tappers” →

Josef Prusa Warns Open Hardware 3D Printing Is Dead

It’s hard to overstate the impact desktop 3D printing has had on the making and hacking scene. It drastically lowered the barrier for many to create their own projects, and much of the prototyping and distribution of parts and tools that we see today simply wouldn’t be possible via traditional means.

What might not be obvious to those new to the game is that much of what we take for granted today in the 3D printing world has its origins in open source hardware (OSHW). Unfortunately, [Josef Prusa] has reason to believe that this aspect of desktop 3D printing is dead.

If you’ve been following 3D printing for awhile, you’ll know how quickly the industry and the hobby have evolved. Just a few years ago, the choice was between spending the better part of $1,000 USD on a printer with all the bells and whistles, or taking your chances with a stripped-down clone for half the price. But today, you can get a machine capable of self calibration and multi-color prints for what used to be entry-level prices. According to [Josef] however, there’s a hidden cost to consider.

Continue reading “Josef Prusa Warns Open Hardware 3D Printing Is Dead” →

A Speed Loader For Your 3D Printer Filament

Reloading filament on a 3D printer is hardly anyone’s favorite task, but it’s even worse when you’re trying to shove stiff filament down a long and winding Bowden tube. Enter the speed loader from [Mr Flippant], which aims to take the pain out of this mechanically-frustrating chore.

The design is simple enough. It’s a small handheld tool that uses a 12 VDC gear motor to drive a set of Bondtech-style drive gears that you might find in an extruder. They’re assembled in a 3D printed housing with a microswitch to activate the motor, and a 9 volt battery to supply the juice.

To use the device, first thread the filament into the beginning of the Bowden tube. The idler gear is on a hinge, such that clamping it into position around the filament with the main gear activates the microswitch and turns the motor on, driving the filament all the way to the extruder. Job done! [Mr Flippant] notes that the filament should be as straight and unkinked as possible for best results, but that’s good advice when 3D printing in general.

Funnily enough, around these parts, when we talk about speed loaders, we’re usually discussing tapes.

Continue reading “A Speed Loader For Your 3D Printer Filament” →

How To Design 3D-Printed Parts With Tolerance In Mind

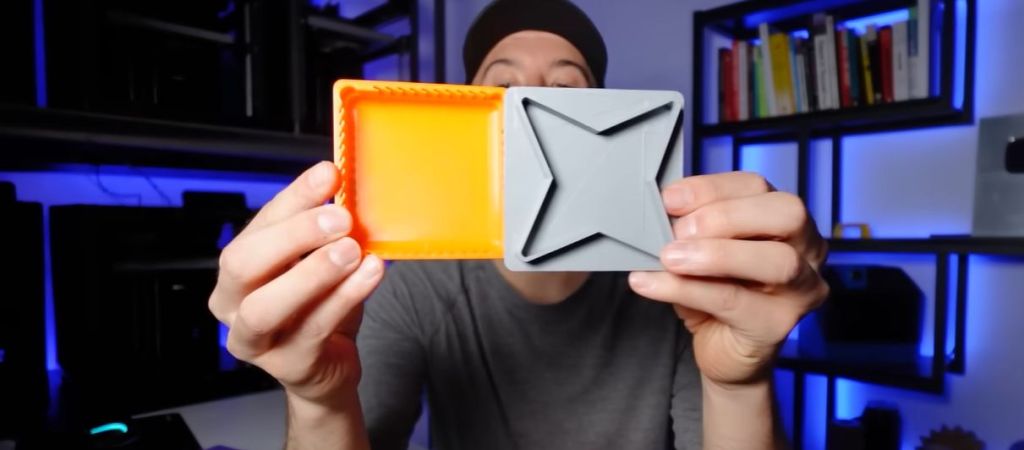
One of the continuing struggles with FDM printing is making sure that parts that should fit together actually do. While adding significant tolerance between parts is an option, often you want to have a friction fit or at least a gap that you cannot drive a truck through. In a video by [Slant 3D] a number of tips and tricks to improve parts design with tolerance in mind are provided.

Starting with the fairly obvious, such as avoiding sharp corners, rounding off edges and using chamfered edges  and filets for e.g. lids to make getting started easy, the video then moves into more advanced topics. Material shrinkage is a concern, which is where using thin walls instead of solid blocks of material helps, as does using an appropriate infill type. Another interesting idea is to use a compliant mechanism in the lid to get a friction fit without getting all print parameters just right.

On the opposing side to the lid – or equivalent part – you’d follow many of the same tips, with the addition of e.g. slots that allow for the part to flex somewhat. All of this helps to deal with any variability between prints, with the suggested grip fins at the end of the video being probably the most extreme.

Continue reading “How To Design 3D-Printed Parts With Tolerance In Mind” →

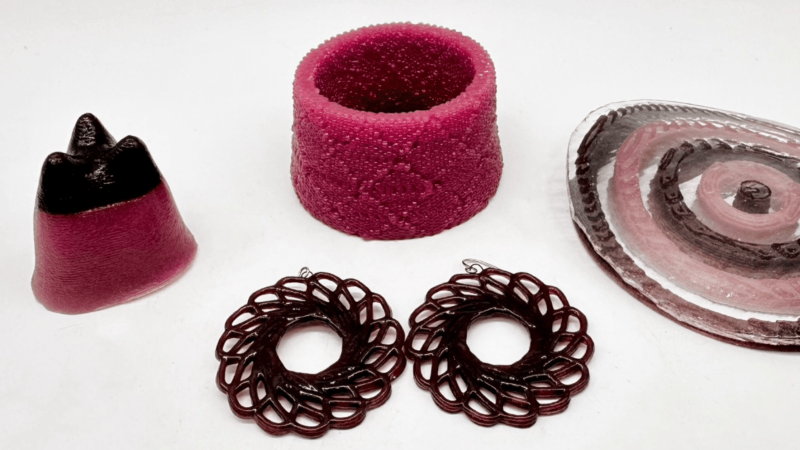
A variety of red and black glass objects are shown on a white background. In the foreground, there are two black spiral-patterned earrings. To the left is a red and black shape with three points on the top. On the right, a deformed glass sheet is shown bent over concentric red and black glass rings. In the center top is a red glass vase with a roughly-textured exterior.

Paste Extrusion For 3D Printing Glass And Eggshells

In contrast to the success of their molten-plastic cousins, paste extrusion 3D printers have never really attained much popularity. This is shame because, as the [Hand and Machine] research group at the University of New Mexico demonstrate, you can use them to print with some really interesting materials, including glass and eggshell. Links to the respective research papers are here: glass and eggshells, with presentations in the supplemental materials.

To print with glass, the researchers created a clay-like paste out of glass frit, methyl cellulose and xanthan gum as shear-thinning binders, and water. They used a vacuum chamber to remove bubbles, then extruded the paste from a clay 3D printer. After letting the resulting parts dry, they fired them in a kiln at approximately 750 ℃ to burn away the binder and sinter the frit. This introduced some shrinkage, but it was controllable enough to at least make decorative parts, and it might be predictable enough to make functional parts after some post-processing.

Path generation for the printer was an interesting problem; the printer couldn’t start and stop extrusion quickly, so [Hand and Machine] developed a custom slicer to generate tool paths that minimize material leakage. To avoid glass walls collapsing during firing, they also wrote another slicer to maintain constant wall thicknesses.

The process for printing with eggshell was similar: the researchers ground eggshells into a powder, mixed this with water, methyl cellulose and xanthan gum, and printed with the resulting paste. After drying, the parts didn’t need any additional processing. The major advantage of these parts is their biodegradability, as the researchers demonstrated by printing a biodegradable pot for plants. To be honest, we don’t think that this will be as useful an innovation for hackers as the glass could be, but it does demonstrate the abilities of paste extrusion.

The same team has previously used a paste printer to 3D print in metal. If you don’t have a paste printer, it’s also possible to print glass using a laser cutter, or you could always make your own paste extruder.